Energy industry

Hoist UK installs a Verlinde-equipped crane for a refrigeration workshop

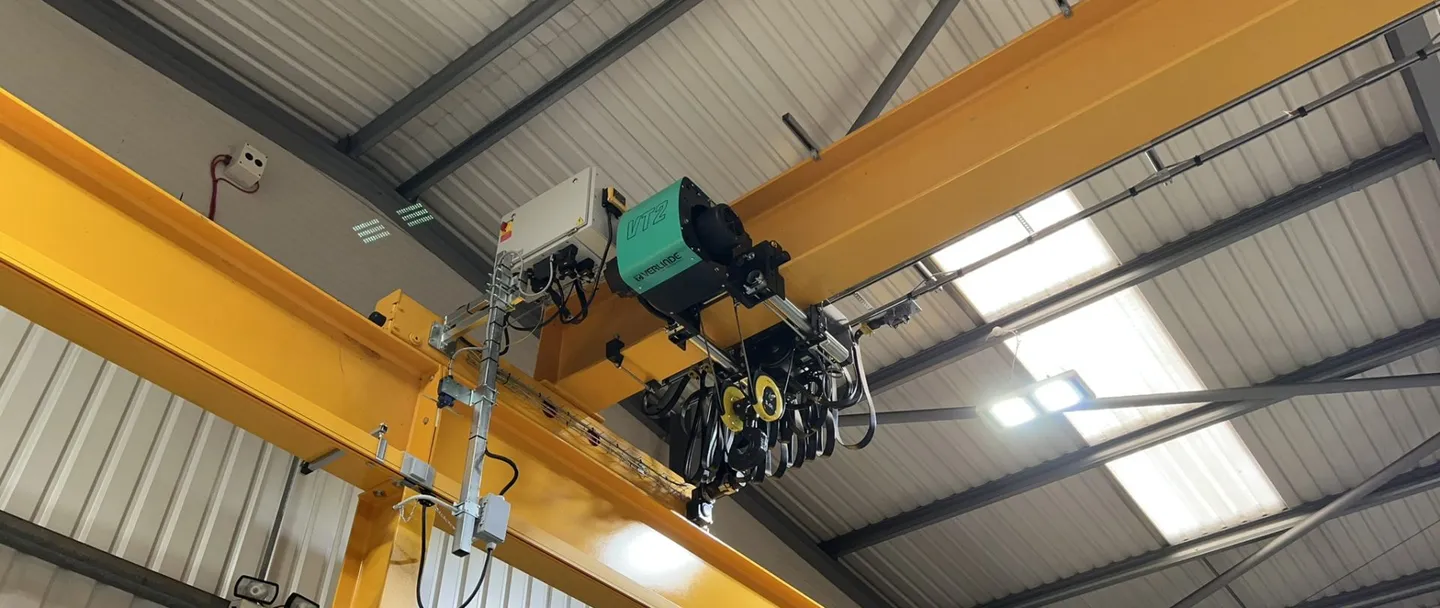
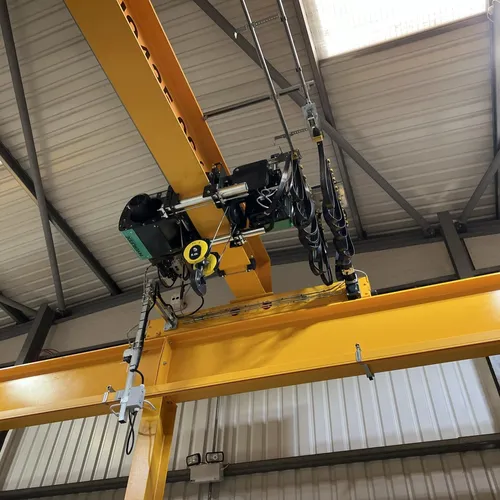
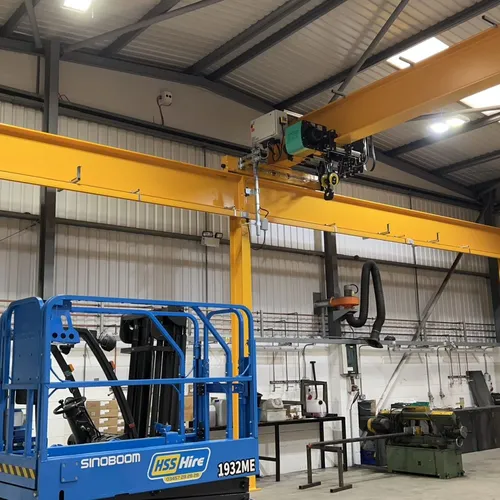
A refrigeration and electrical contractor turned to Hoist UK, a long-standing and trusted Verlinde partner, for an overhead lifting solution in its newly occupied fabrication workshop. The customer needed complete workshop coverage to support general fabrication and assembly activities while maintaining unrestricted forklift access beneath the crane structure. Hoist UK delivered a complete overhead lifting solution equipped with Verlinde VT2 wire rope hoist.

Industry
Industrial refrigeration
Location
United Kingdom
Products
Verlinde VT2 wire rope hoist

OVERVIEW AND CHALLENGE


The primary design consideration was achieving maximum crane coverage across the workshop while maintaining clear access for forklift movement throughout the building.

To meet this requirement, Hoist UK carefully designed the gantry steelwork around the existing building layout. Compound columns were engineered to eliminate the need for bracing between the legs, allowing unrestricted travel beneath the runway structure. Precise site measurements and design coordination were required to ensure that the crane system fitted within the available space while delivering optimal lifting height and operational efficiency.


SOLUTION


Hoist UK supplied and installed a top-running overhead crane equipped with Verlinde VT2 wire rope hoist. The crane was specified with a rated capacity of 5,000 kg and a span of 10.8 metres, operating on a 16.7-metre runway. The freestanding gantry steelwork was manufactured in-house by Hoist UK and designed specifically to suit the customer’s building layout. The structure had a height of approximately 4.85 metres and provided a lifting height of approximately 4.67 metres.


The Verlinde VT2 hoist provided dual hoisting speeds of 4 and 0.7 metres per minute, delivering true vertical lift through a 4-fall reeving arrangement. Cross-travel speeds of 5 and 20 metres per minute and long-travel speeds of 8 and 32 metres per minute were achieved using inverter-controlled variable-speed drives, allowing smooth and controlled movement of the load.


The crane was supplied with radio control for wireless operation, together with a “plug-and-play” back-cabled pendant system. Long-travel and cross-travel limit switches were incorporated to provide controlled slow-down and stop functions.


The freestanding gantry legs were secured to the existing concrete floor using resin anchors.

Results and key benefits

  • Full lifting coverage across the fabrication workshop.

  • Efficient material handling without disrupting forklift operations.

  • A flexible and space-efficient solution tailored to the customer’s fabrication and assembly activities

  • A 5,000 kg top-running crane equipped with a Verlinde VT2 wire rope hoist.

  • Variable-speed travel, radio control and limit switches for smooth and precise operation.

  • A custom freestanding gantry with compound columns, designed and manufactured in-house by Hoist UK.

Be the first to know.

Get Verlinde's latest product launches, certifications and industry news delivered directly to your inbox.

By subscribing, you agree to receive Verlinde news by email. Read our data protection policy.

Other case studies

See all case studies
Energy industry

Verlinde PDW winch supports high-performance wood chip handling

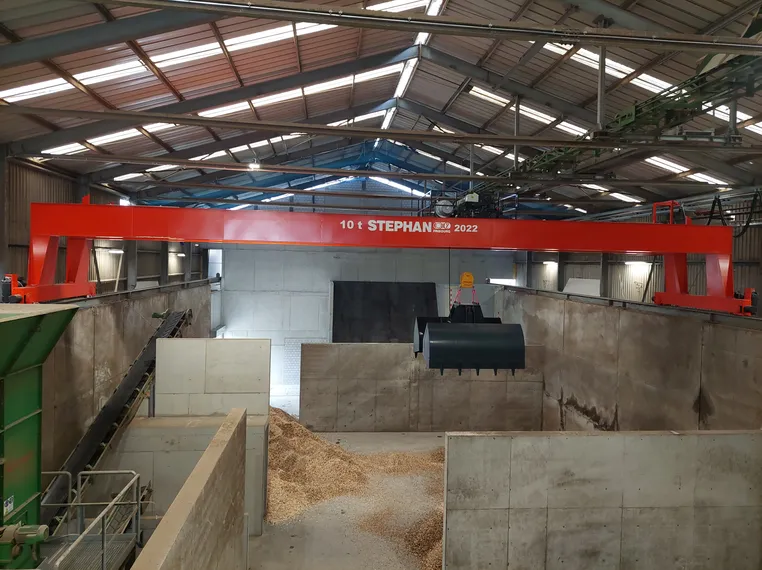
STEPHAN, a Swiss specialist in structural steelwork and lifting equipment, designed an automated overhead travelling crane for a wood chip processing facility. Equipped with a Verlinde PDW open winch, the crane handles sustained operating cycles, long travel distances and high speeds while lifting loads of up to 10 tonnes.
Energy industry

Two Synchronized Verlinde Hoists for Precision Lifting

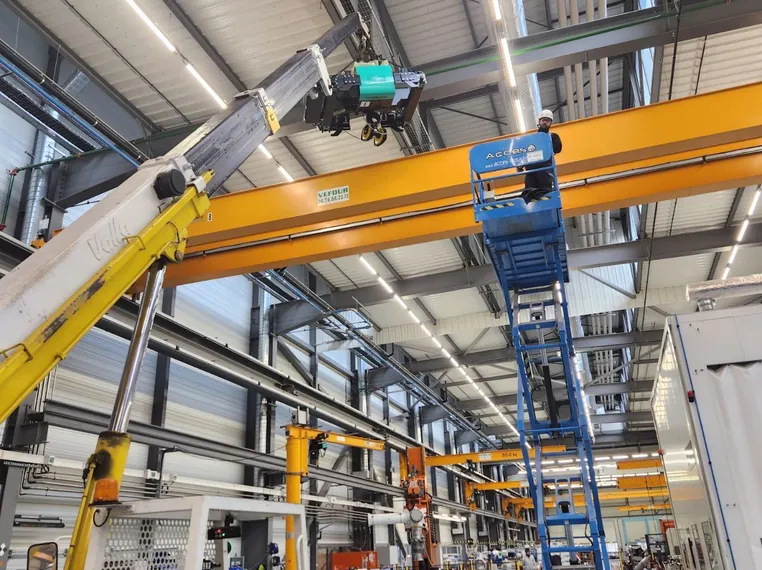
CIC ORIO Vefour has integrated a second Verlinde Eurobloc VT3 wire rope hoist onto an existing overhead crane. The installation aimed to facilitate the synchronised lifting of long and fragile tubular parts using dual hooks, in compliance with standard EN 15011, which mandates simultaneous stopping at the end of travel and load summation.

Manufacturing industry

SERE Maintenance equips Manitou Group’s new production unit with 15 overhead cranes

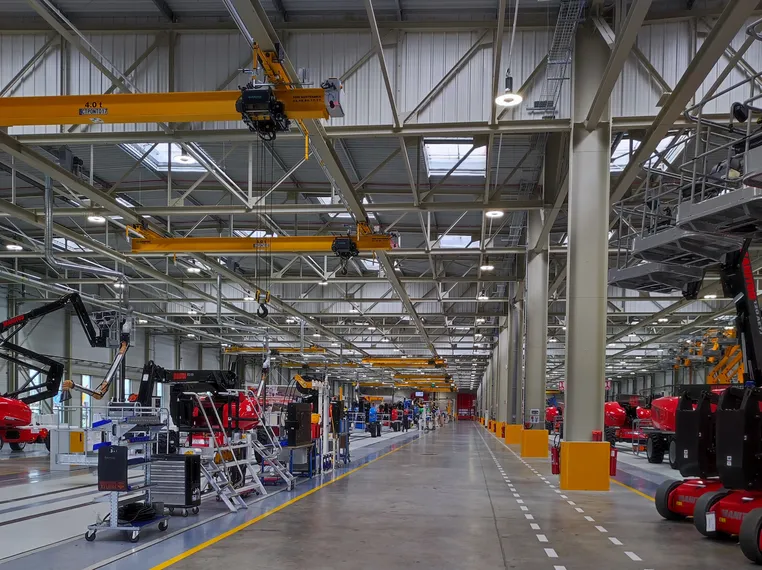
SERE Maintenance, designer and manufacturer of lifting equipment, handling systems and overhead cranes, equipped Manitou Group’s new rough-terrain aerial platform production unit in Candé with 15 custom-designed overhead cranes. A member of the EUROPONT and SAV Verlinde networks, SERE Maintenance adapted the lifting equipment to the factory’s dimensions, assembly lines and safety requirements

Let's find the right solution together.